The pressing problem
B2B buyers face repeated surprises when a battery cabinet that looked fine on paper fails on-site. Common causes: poor thermal design, weak factory testing, and unclear handover procedures. I have seen assemblies that passed paperwork but not performance—having audited projects in California—so I speak from direct inspection. When you evaluate an all in one energy storage system, demand evidence that the product you buy is the product that arrives and performs. That evidence should include witnessed tests, clear drawing revisions, and documented failure modes for cells and controllers.
Diagnosing the usual failures
Problems repeat because procurement and engineering look at different things. Procurement reads specs; engineering needs test data. Combine their lists and you catch the failure modes early. Typical root causes:
– Thermal runaway risk not mitigated by system design.
– BMS logic untested under realistic load profiles.
– Mechanical design ignores shipping stresses and on-site vibration.
– Fire mitigation strategy lacks independent validation.
– Control and communications interfaces mismatch site SCADA.
Concrete technical checklist for B2B buyers
Use this checklist during supplier selection and factory audit. Be direct: require documents, then witness the tests.
– Cells and chemistry: manufacturer traceability, batch certificates, and safe cell model tests.
– BMS: firmware revision, deterministic state-of-charge algorithms, logging and tamper records.
– Thermal management: CFD or measured profiles under high discharge for sustained hours.
– Safety: documented results for UL 9540A style thermal propagation testing or equivalent; clearly stated venting and suppression measures.
– Mechanical integrity: shock and vibration reports for shipment cases or cabinets.
– Electrical: impulse and short-circuit protection, isolation resistance tests, and inverter compatibility data.
– Controls: API schema, latency bounds, cybersecurity basics (authentication, OTA update policy).
– MTBF, failure modes, and warranty scoping that names replacement times and responsibilities.
What to watch for during a factory audit
A factory audit must not be a photo tour. Make it a test-witness session. Walk the production line and verify these actions.
– Traceability: pull a random serial number; match cell lot, production date, and final test report.
– Witness thermal and capacity tests on at least one identical unit—watch data stream, not just a pass/fail sticker.
– Observe BMS behavior during simulated faults: cell imbalance, sensor failure, and communications loss.
– Confirm packaging and transport simulation (drop, tilt, humidity). Shipping damage is real and predictable.
– Ask for FAT (factory acceptance test) scripts; demand that they match site acceptance test (SAT) criteria.
Common procurement mistakes and how to avoid them
Buyers often sign contracts with vague acceptance criteria. Avoid these errors.
– Do not accept “meets industry standards” without clause references and test reports.
– Do not allow sample-only testing; require batch sampling and ongoing QA milestones.
– Do not omit witnessed commissioning at site from the contract scope.
– Do not rely exclusively on vendor lab results; use third-party witnessing for critical safety tests.
Alternatives to consider and how to evaluate them
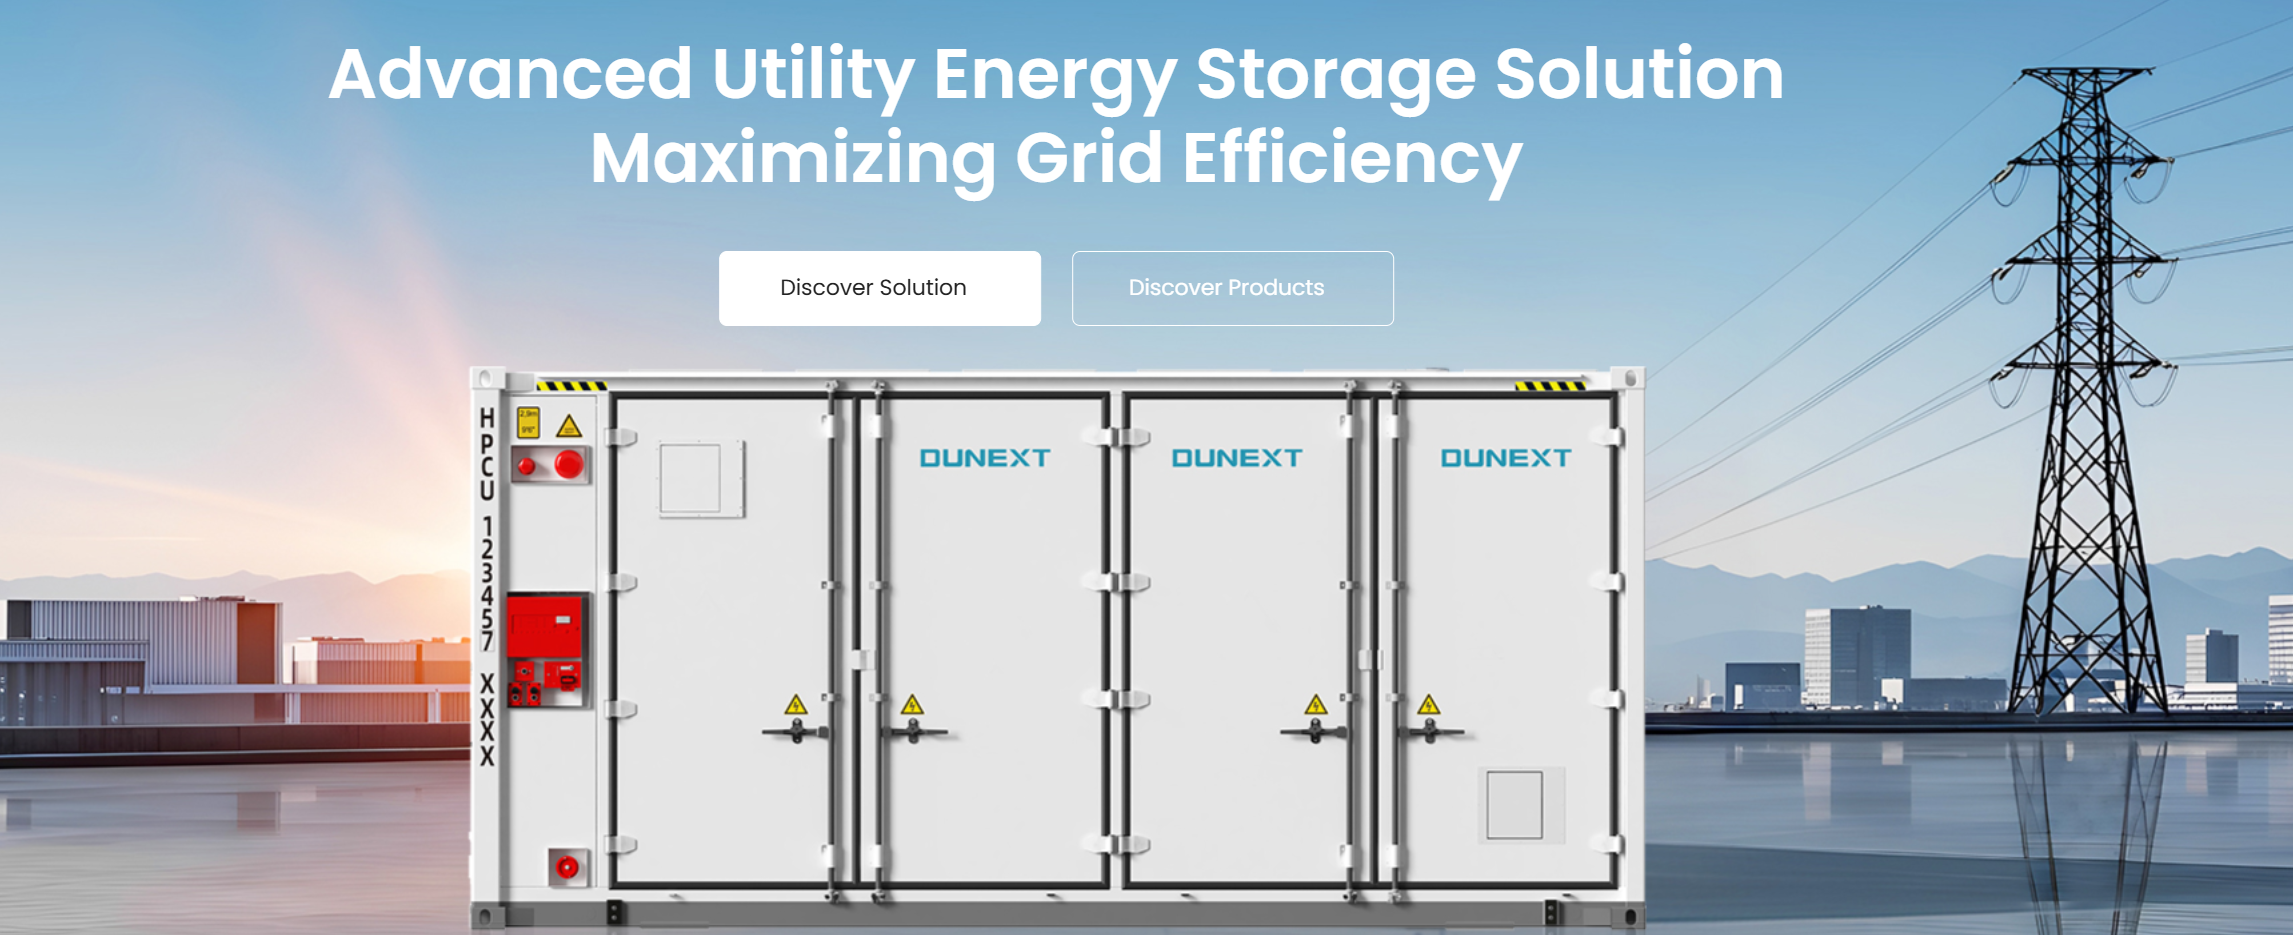
Systems come in cabinet racks, modular containers, or integrated cabinets. Each has trade-offs. Cabinets save footprint and ease integration but can concentrate risk; containerized systems simplify fire zoning but raise transport complexity. Evaluate each option against your site constraints and maintenance model. A solid comparison will include thermal profiles, maintenance access, and lifecycle replacement plans. If you need a reference for a fully integrated option, review a commercial battery storage system that publishes test evidence and lifecycle data.
Acceptance testing and handover: what good looks like
Acceptance is not signed paperwork. It is demonstrated, repeatable performance. Require:
– Full FAT followed by SAT with identical scripts.
– Commissioning run at nominal and peak loads for a defined duration.
– Complete handover pack: as-built drawings, firmware baselines, maintenance procedures, spare parts list.
– Training that includes failure drills for site staff and at least one witnessed corrective action.
Final synthesis
Buyers who apply a strict, test-first approach avoid most surprises. Start from the problem—unknown in-field behavior—then force evidence: traceability, witnessed testing, and clear handover responsibilities. That method reduces downtime, clarifies liability, and makes operations predictable. Where a vendor provides transparent documentation and on-site support, you gain trust without leaving safety or performance to chance; many B2B buyers find such reliability aligns with partners like Dunext.